The Physics of Photon Burning: How CO2 Lasers Transform Wood
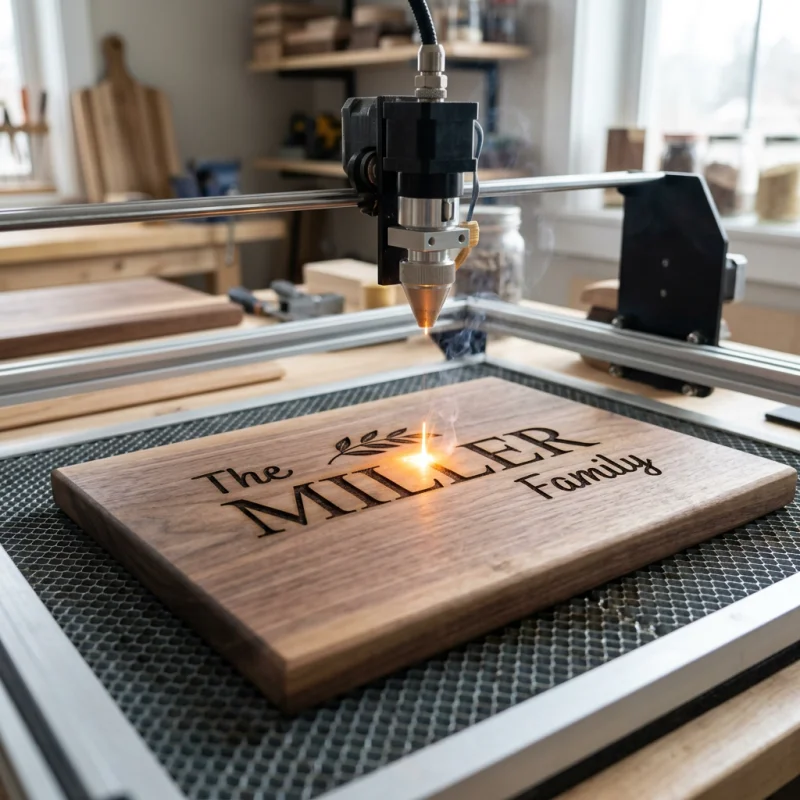
A focused beam of invisible light strikes a raw maple cutting board. Within microseconds, the surface temperature surges past 300°C. Cellulose chains break apart, releasing volatile gas while leaving behind sharp carbonized lines. That is the core mechanics of co2 laser wood engraving.
The 10.6-Micron Wavelength and Wood Photons
CO2 laser tubes produce infrared light at a wavelength of 10.6 micrometers (10,600 nanometers). Human eyes cannot detect this spectrum. Wood, however, absorbs it almost completely.
Organic timber consists primarily of cellulose structural fibers bound together by lignin. These complex polymers contain carbon-hydrogen and carbon-oxygen molecular bonds. They resonate at the exact vibrational frequency corresponding to 10.6-micron light. When photons at this wavelength hit timber, molecular vibration instantly spikes. The material bypasses melting (wood doesn't melt) and transitions directly from solid state to thermal decomposition, known as pyrolysis.
At temperatures between 200°C and 260°C, hemicellulose breaks down. By 280°C to 500°C, cellulose rapidly decomposes, shedding water vapor and carbon monoxide. What stays behind in the beam path is fixed carbon. This carbonized residue creates the dark, precise marks visible on custom wooden journal covers and personalized gifts.
Beam Optics, Spot Size, and Energy Density
Raw laser beams exiting a glass tube or RF metal tube measure roughly 2mm to 7mm in diameter. A beam that wide is too diffuse to engrave tight typography or intricate line work. Passing the light through a zinc selenide (ZnSe) focal lens squeezes those photons down to a focal spot diameter between 0.1mm and 0.2mm.
Focusing compresses energy into a microscopic footprint. This drastically increases power density, measured in Watts per square centimeter (W/cm²). A 60-Watt CO2 laser focused to a 0.15mm spot generates a power density exceeding 340,000 W/cm² at the focal point.
Understanding how co2 lasers work on wood requires looking at pulse frequency, measured in Hertz (Hz) or pulses per inch (PPI). High-frequency pulsing creates smooth, continuous channels without leaving visible perforation dots along vector paths.
Technical Specifications Across Laser Source Types
Different laser light sources interact with raw timber in fundamentally distinct ways. Comparing their key specs reveals why specific machines excel at distinct tasks.
| Parameter | CO2 Laser (10.6 µm) | Diode Laser (450 nm) | Fiber Laser (1064 nm) |
|---|---|---|---|
| Primary Wavelength | 10,600 nm | 450 nm | 1,064 nm |
| Focal Spot Diameter | 0.10 mm – 0.20 mm | 0.08 mm – 0.15 mm | 0.01 mm – 0.05 mm |
| Cellulose Absorption Rate | 90% – 95% | 30% – 50% | Under 10% |
| Typical Optical Power | 40W – 150W | 5W – 40W | 20W – 100W |
| Engraving Speed on Hardwood | 300 – 600 mm/s | 20 – 80 mm/s | Unsuitable for bare wood |
| Heat-Affected Zone (HAZ) Width | 0.05 mm | 0.30 mm | N/A (passes through) |
Wavelength Matching: Why CO2 Dominates Hardwood Gifts
Near-infrared fiber lasers (1064 nm) work exceptionally well on metals because free electrons absorb short infrared energy readily. Bare wood acts almost like clear glass to a fiber laser; photons pass straight through without generating enough heat to pyrolyze the surface.
Blue diode lasers (450 nm) can mark wood because organic pigments absorb visible blue light. However, their limited optical wattage forces machines to run at low speeds. Slow passes allow thermal energy to bleed sideways into surrounding wood fibers, leaving soft, blurred edges instead of crisp typography.
CO2 units deliver energy absorption rates over 90% across American walnut, cherry, and hard maple. Higher speeds mean shorter dwell time at any single coordinate, trapping heat within a tightly controlled zone. You get dark graphic lines without charring adjacent timber grain.
Material Limitations and Safety Risks
While CO2 systems process organic timber effectively, specific material properties present clear hazards and operational boundaries.
- High-Resin Softwoods: Woods like knotty pine and cedar contain heavy pockets of sap and volatile resins. When hit by a 10.6-micron beam, these resins boil and flare up, igniting open flames that scorch the surface and coat mirrors with sticky film.
- Reflective Metal Inlays: Brass or aluminum accents reflect 10.6-micron energy straight back into the optic path. This feedback shatters costly ZnSe lenses within milliseconds.
- Synthetic Glues in Low-Grade Composite Boards: Interior-grade plywood and MDF use urea-formaldehyde binders. Laser vaporization breaks down these adhesives, off-gassing toxic fumes that demand high-cubic-feet-per-minute exhaust extraction.
- Thermal Warping on Thin Sheets: Veneers under 1.5mm thick distort quickly under heavy raster filling. Counteract this warping by setting air assist pressure to 30 PSI, which chills the work zone while driving away soot particulate.
Why does walnut engrave darker than birch or maple?
Walnut contains rich concentrations of natural tannins and complex organic compounds that carbonize into dark brown and black pigments at 300°C. Lighter woods like birch have lower natural resin density, leaving golden-tan marks unless power density is increased or head speed is reduced.
How does air assist pressure affect engraving quality?
Air assist streams compressed air (typically 15 to 30 PSI) directly down through the nozzle cone onto the focal point. This air stream suppresses open flames, clears smoke out of the beam path before it can scatter photons, and blows excess carbon dust off the timber face.
Can a CO2 laser engrave clear-coated or varnished wooden gifts?
Yes. The beam vaporizes polyurethane and lacquer topcoats clean off during the first pass. However, synthetic varnishes generate irritating fumes that require active exhaust filters. Organic food-safe finishes like mineral oil or beeswax don't block photon absorption or release harsh fumes.
What causes burnt, blurry edges around engraved text?
Blurry edges happen when laser power density drops or travel speed is set too slow. That combination lets heat bleed laterally through timber fibers beyond the target zone. An out-of-focus lens or weak air assist pressure also spreads heat wider than the intended 0.1mm spot.